 Sep 17, 2026
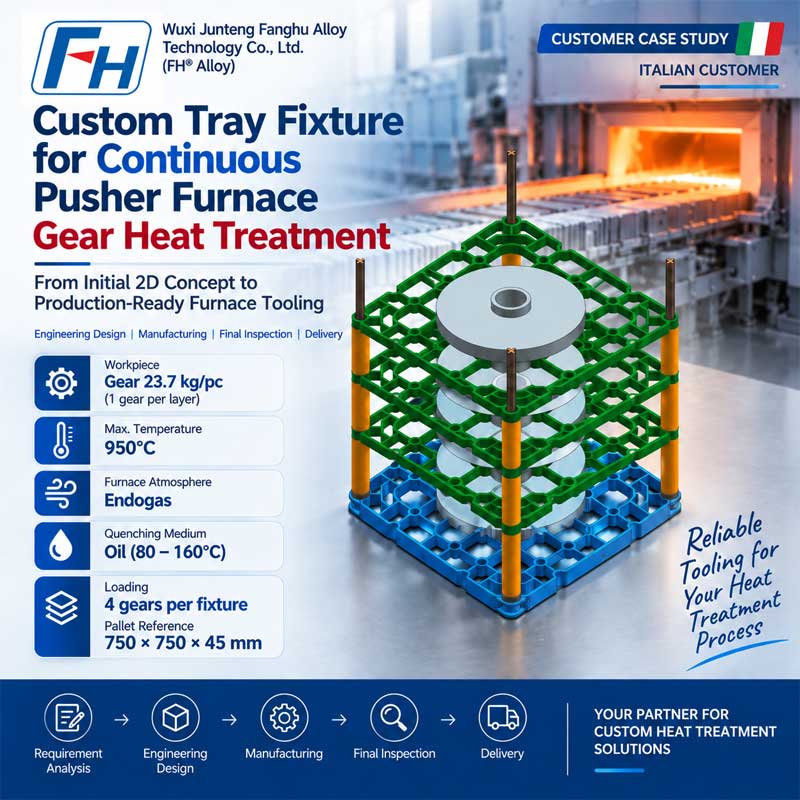
Custom Tray Fixture System for Continuous Pusher Furnace Gear Heat Treatment
Customer Case Study | Engineering Design, Drawing Approval, Manufacturing & Delivery
Product: Custom Heat Treatment Tray Fixture System
Furnace Type: Continuous Pusher Furnace
Application: Chemical-Thermal Treatment of Gears
Furnace Atmosphere: Endogas
Maximum Temperature: 950°C
Quenching Medium: Oil, 80–160°C
Workpiece: Gear, approx. 23.7 kg/pc
Loading: 4 gears per fixture
Initial Tray Reference: 750 × 750 × 45 mm
Loading / Unloading: Manual
Preliminary Quantity: 40 sets
Manufacturer: Wuxi Junteng Fanghu Alloy Technology Co., Ltd. (FH® Alloy)
Project Overview
FH® Alloy received an inquiry for a customized heat treatment tray fixture system to be used in a continuous pusher furnace for chemical-thermal treatment of gears.
The customer had an initial 2D concept and application sketch, but the drawings were not complete enough for direct production.
Instead, they asked FH® Alloy to use our furnace tooling experience to determine and optimize:
A complete engineering drawing was required for the customer’s end user to review and approve before production.
After technical evaluation, FH® Alloy completed the fixture design, prepared the required drawings, proceeded with manufacturing after approval, performed final quality inspection, and delivered the finished tooling.
This project therefore involved much more than simple build-to-print manufacturing.
It was a complete:
Application Review → Engineering Design → Drawing Approval → Manufacturing → Inspection → Delivery
Customer Operating Conditions
The customer provided detailed heat treatment information to support the fixture design.
| Item | Customer Requirement |
| Furnace Type | Continuous Pusher Furnace |
| Process | Chemical-Thermal Treatment |
| Furnace Atmosphere | Endogas |
| Maximum Temperature | 950°C |
| Quenching Medium | Oil |
| Oil Temperature | 80–160°C |
| Main Workpiece | Gear |
| Gear Weight | Approx. 23.7 kg/pc |
| Gears per Fixture | 4 pcs |
| Initial Tray Reference | 750 × 750 × 45 mm |
| Loading Method | Manual |
| Unloading Method | Manual |
| Preliminary Quantity | Approx. 40 sets |
These parameters formed the basis for FH® Alloy’s engineering design.
Customer Needed More Than a 2D Drawing
One of the key features of this project was that the customer already had a basic sketch, but still required FH® Alloy to develop the complete production-ready fixture design.
The customer specifically asked FH® Alloy to use our practical supply experience to determine an appropriate configuration for:
The completed engineering drawing then needed to be submitted to the customer for approval.
This is different from conventional OEM production where the supplier simply follows a finalized drawing.
For this project, FH® Alloy participated directly in the engineering stage.
Engineering Challenge
The tooling had to work reliably under several demanding conditions.
1. Continuous Pusher Furnace Operation
In a pusher furnace, trays and fixtures are repeatedly moved through the furnace line.
The tooling therefore needs to consider:
The structure must be suitable not only for high temperature, but also for repeated production cycles.
2. Gear Loading
Each processed gear weighed approximately:
23.7 kg
The customer intended to load:
4 gears per fixture
This meant the basic workpiece weight was approximately:
94.8 kg per loading unit
before considering the weight of the fixture itself.
FH® Alloy therefore needed to evaluate the supporting positions and tray structure so that the gears could be loaded securely and the weight distributed effectively.
3. 950°C Endogas Atmosphere
The fixture was intended for chemical-thermal treatment at temperatures up to:
950°C
in an endogas atmosphere.
At this temperature, furnace tooling must maintain adequate high-temperature strength and dimensional stability throughout repeated production cycles.
The casting material and structural sections therefore needed to be selected together rather than independently.
4. Oil Quenching at 80–160°C
After heat treatment, the tooling is exposed to oil-quenching conditions.
The customer specified an oil temperature range of:
80–160°C
This large temperature change from furnace operation to quenching creates thermal stress in the tooling.
For this reason, FH® Alloy considered:
during the engineering stage.
Proposed Fixture Structure
According to the customer’s initial concept, one rack system included multiple key components.
These included:
Base Trays
The customer’s initial reference indicated a tray size of approximately:
750 × 750 × 45 mm
FH® Alloy reviewed the tray geometry according to the gear loading and furnace conditions.
Vertical Guides
The initial rack concept included:
4 vertical guides
These guides help maintain the relative position of the stacked fixture components and support the overall arrangement during loading and furnace operation.
Intermediate Bushings
The customer’s concept included:
12 intermediate bushings
FH® Alloy evaluated the bushing arrangement together with the vertical supports and tray structure to ensure practical assembly and spacing.
Optimizing for Manual Loading and Unloading
The customer specifically indicated that the fixtures would be loaded and unloaded manually.
This was an important design input.
The tooling therefore needed to consider not only furnace performance, but also operator usability.
FH® Alloy reviewed:
The objective was to provide sufficient structural strength without making the loading process unnecessarily difficult.
Material Selection Support
The customer also asked FH® Alloy to recommend a suitable casting material based on our experience.
For heat treatment tooling, material selection should consider:
FH® Alloy therefore evaluated the material together with the final design rather than treating material choice as a separate purchasing decision.
This type of engineering support is especially important when a customer has process data but has not yet finalized the furnace tooling specification.
From Initial Sketch to Complete Engineering Drawing
The customer required FH® Alloy to provide drawings for technical approval before production.
The project workflow was therefore:
Customer 2D Concept / Operating Data
↓
Process & Load Analysis
↓
Tray and Rack Structure Development
↓
Guide & Bushing Optimization
↓
Material Evaluation
↓
Complete Engineering Drawing
↓
Customer / End-User Review
↓
Production Approval
This approval stage reduced the risk of misunderstanding before manufacturing and ensured that the production tooling matched the customer’s application requirements.
Customer Confidence in FH® Alloy’s Engineering Capability
An important part of this project was the customer’s expectation that FH® Alloy would contribute engineering experience rather than only provide a quotation.
The customer specifically asked us to help select:
They also expressed confidence in FH® Alloy’s experience in supplying heat treatment tooling and requested our engineering drawings for their customer’s technical approval.
This demonstrates the role FH® Alloy can play as an engineering and manufacturing partner, rather than only a component supplier.
Manufacturing
After the design and drawings were approved, FH® Alloy proceeded with production of the fixture system.
Manufacturing was carried out according to the final engineering drawings, with particular attention to:
For a multi-component system like this, dimensional control is especially important because all parts must work together during loading and furnace operation.
Final Quality Inspection
Before shipment, FH® Alloy carried out final inspection of the finished tooling.
Quality control included:
Dimensional Inspection
Checking the main dimensions against the approved production drawings.
Structural Inspection
Inspecting trays, guides, supports and connecting components.
Assembly Compatibility
Confirming that the individual components fitted together correctly as a complete rack system.
Drawing Conformity
Verifying that the finished products matched the customer-approved engineering design.
After the products passed final inspection, they were prepared for shipment.
Project Specifications
| Item | Specification |
| Product | Heat Treatment Tray Fixture System |
| Furnace Type | Continuous Pusher Furnace |
| Application | Chemical-Thermal Treatment of Gears |
| Atmosphere | Endogas |
| Maximum Temperature | 950°C |
| Quenching | Oil |
| Quenching Oil Temperature | 80–160°C |
| Gear Weight | Approx. 23.7 kg/pc |
| Loading | 4 gears per fixture |
| Workpiece Load | Approx. 94.8 kg per fixture |
| Initial Tray Reference | 750 × 750 × 45 mm |
| Loading / Unloading | Manual |
| Main Components | Trays + Vertical Guides + Intermediate Bushings |
| Preliminary Quantity | Approx. 40 sets |
| Drawing Status | Customer supplied initial concept; complete drawings developed by FH® Alloy |
| Project Scope | Design → Approval → Production → Inspection → Delivery |
Project Highlights
Engineering Beyond Build-to-Print
The customer had an initial 2D concept, but FH® Alloy was responsible for developing the complete production-ready tooling drawings.
Designed Around Real Process Conditions
The fixture design considered:
950°C + Endogas + Oil Quenching + Gear Load + Manual Handling
rather than simply following external dimensions.
Complete Rack System
The project involved not only trays, but also:
Customer Approval Before Production
FH® Alloy provided complete technical drawings for the customer and end user to review before manufacturing.
Full Project Execution
The project covered:
Engineering Design → Drawing Approval → Manufacturing → Final Inspection → Delivery
Why Choose FH® Alloy for Pusher Furnace Tooling?
Wuxi Junteng Fanghu Alloy Technology Co., Ltd. (FH® Alloy) designs and manufactures customized furnace tooling for industrial heat treatment applications, including:
We can work from:
Need a Fixture Designed from Your Process Conditions?
You do not necessarily need a complete tooling drawing before contacting FH® Alloy.
For engineering evaluation, you can provide:
FH® Alloy can then support:
Application Review → Fixture Design → Complete Drawing → Manufacturing → Inspection → Delivery
About FH® Alloy
Wuxi Junteng Fanghu Alloy Technology Co., Ltd. (FH® Alloy) specializes in customized heat treatment fixtures and high-temperature alloy components for industrial furnace applications.
Our capabilities cover engineering design, heat-resistant alloy casting, machining, assembly and customized furnace tooling production.
Engineering Design | Custom Manufacturing | Heat Treatment Furnace Solutions
 CategoryRecent Post

Focus on Designing and Manufacturing Alloy Steel Parts since 2006
 Tel: 0510-83310100
 E-mail: info@alloy-casting.com
 Office Add: Room 1105,Building 6, Jiaye Wealth Center,Wuxi, Jiangsu, P.R.China P.C.:214000.
 Privacy

 English
 Español
 italiano
 Deutsch
 0086-13338774804
